Quick Answer
Solid PTFE balls are made by compression molding virgin resin at 20–25 MPa, sintering in ovens up to 370°C, then turning and centerless grinding to final diameter — not by injection molding. Every batch is dimensionally inspected before dispatch.
The Journey from Polymer Powder to Precision Sphere
The manufacturing process for solid PTFE balls involves three core stages: cold compaction molding, controlled thermal sintering, and centerless grinding/turning. Because PTFE cannot be injection-molded due to its high melt viscosity, fine-cut polymer powder is compacted at 20-25 MPa to form preforms, sintered at 370°C to fuse molecular chains, and centerless ground to achieve precision tolerances down to ±0.05 mm. This guide provides an in-depth explanation of the steps involved in producing solid PTFE spheres at HEMSUN ENGG. INDUSTRIES’ Gandhinagar plant.
Step 1: Raw Material Selection and Compounding
The manufacturing process begins with the selection of high-purity virgin PTFE resin powders. We utilize industry-standard resins such as SRF Flonio 120/210 and GFL Inoflon 610 (see Virgin PTFE Balls details). These fine-cut polymer powders must be kept in temperature-controlled, dust-free environments to prevent contamination. If the final application requires enhanced mechanical properties—such as increased wear resistance, lower thermal expansion, or higher load-bearing capacity—fillers like glass fibers, carbon powder, graphite, molybdenum disulfide (MoS2), or bronze powder are compounded with the virgin resin in precise ratios using high-shear blenders to produce specialized Custom PTFE Balls compounds.
Step 2: Preform Compression Molding
Because PTFE cannot flow through runner systems, the raw powder is loaded into custom-designed steel mold dies fabricated in our in-house toolroom. The molds are shaped to create cylindrical or spherical preforms (also known as green billets) that are slightly larger than the target ball diameter. The powder is compacted at room temperature using hydraulic presses. The compaction pressure is highly critical and must be carefully controlled between 20 and 25 MPa (Megapascals). If the pressure is too low, the preform will contain microscopic air voids, leading to porosity and leakage under pressure. If the compaction pressure is too high, the polymer particles can shear, creating structural planes that fail during sintering. The result is a compacted “green” preform that has sufficient mechanical strength to be handled but is not yet fully fused.
Step 3: Controlled Oven Sintering
To fuse the compacted polymer particles into a dense, continuous plastic structure, the green preforms undergo a thermal sintering process. The preforms are placed into high-precision, programmable industrial ovens. The sintering cycle is slow and carefully managed, often lasting between 12 to 24 hours depending on the billet volume. The temperature is gradually ramped up at a rate of 20°C to 45°C per hour until it exceeds the crystalline melting point of PTFE, reaching approximately 360°C to 380°C. At this temperature, the polymer transition occurs, and the white compacted powder becomes gel-like as the particles fuse together. The temperature is held at this peak for several hours to ensure complete thermal equilibrium. Next, the cooling cycle begins. The cooling rate must be strictly controlled (typically 15°C to 30°C per hour) to manage the degree of polymer crystallinity, which directly influences the ball’s final density, tensile strength, and dimensional stability.
Step 4: Precision Machining
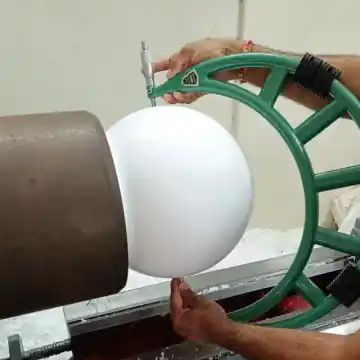
Once the sintered PTFE billets are cooled to room temperature, they are ready for machining. Sintered billets are mounted onto dedicated automatic lathes and ball turning machinery. The rough billet is machined into a sphere using specialized radius-cutting tools. Because PTFE has a high coefficient of thermal expansion and is relatively soft, the machining tool geometry, feed rate, and spindle speed must be optimized to prevent heat buildup, which can cause the material to expand during cutting and lead to incorrect dimensions after cooling. Sharp carbide tools and constant chip extraction are used to achieve the target nominal diameter.
Step 5: Centerless Grinding and Finishing
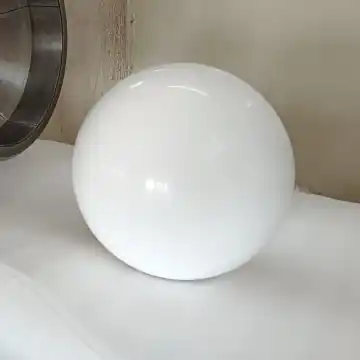
To meet the tight dimensional and roundness tolerances required for leak-free valve applications, the machined spheres undergo centerless grinding and polishing. The balls are fed between a grinding wheel and a regulating wheel in a wet grinding system. This process systematically removes high spots, bringing the ball to its final diameter and ensuring a high degree of spherical roundness (often achieving tolerances down to ±0.05 mm on smaller sizes; refer to our PTFE Ball Sizes table). The final step is polishing, where the balls are tumbled with fine abrasive media to achieve a smooth surface finish (typically Ra < 0.4 microns), which is essential for ensuring a tight seal against soft valve seats.
Step 6: Inspection, Quality Control, and Dispatch
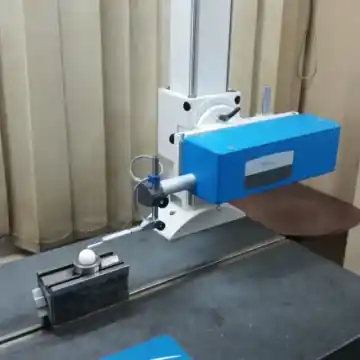
Every batch of finished PTFE balls is subjected to strict quality control inspections. We verify:
-
Dimensional Accuracy: Measured using calibrated digital micrometers and coordinate measuring machines (CMM).
-
Spherical Roundness: Checked using roundness testers to ensure the sphere does not have flat spots.
-
Porosity and Voids: Monitored via specific gravity testing to confirm the density matches the target 2.15–2.18 g/cm³ range.
-
Visual Surface Quality: Inspected under magnification for scratches, pits, or embedded contaminants.
Once approved, the balls are washed, packed in anti-static polybags, boxed in shock-absorbing cartons, and dispatched with material test certificates (MTC) showing compliance with specifications.
Hollow PTFE Balls — Separate Manufacturing Path
Solid and hollow PTFE balls are both manufactured in-house, but hollow spheres use a different construction method. For PTFE hollow balls, we mold two matched virgin PTFE hemispheres in dedicated dies, prepare the equatorial mating faces, and join them using controlled thermal fusion and chemical welding — not a snap-fit or adhesive-only joint. After welding, the outer diameter, wall thickness, and sphericity are finished on lathes and grinders. Hollow construction lowers mass versus a solid sphere of the same outer diameter, making these balls well suited to rotameter floats, level indicators, and buoyancy assemblies. Share your outer diameter, wall thickness, or displacement target for a factory quote.
In-depth engineering analysis and parameter breakdown
Achieving consistent, high-yield production in ptfe ball manufacturing process explained requires precise control over raw material physical chemistry, hydraulic compaction parameters, thermal heating/soaking curves, and tool steel metallurgical properties.
Key Engineering Parameter Matrix
| Process Variable | Standard Engineering Tolerance | Impact on Component Integrity | Monitoring & Verification Method |
|---|---|---|---|
| Compaction Pressure | 300 to 500 kg/cm² (3,000–4,500 psi) | Determines preform green density (target 2.14–2.18 g/cm³); prevents porosity | Digital hydraulic pressure transducer on primary ram cylinder |
| Pressure Dwell Duration | 15 seconds to 5 minutes | Eliminates trapped air pockets and enables particle interlocking | Automated PLC cycle timer with linear scale position hold |
| Tooling Cavity Clearance | 0.025 mm to 0.040 mm per side | Allows air bleeding while preventing powder flash along punch seams | Precision ground punches and CMM-verified die bores |
| Sintering Peak Temperature | 365°C to 375°C (±3°C uniform) | Ensures complete molecular coalescence across the crystalline melting point | Multi-zone thermocouple array with PID digital controller |
| Recrystallization Cooling Rate | 30°C to 45°C per hour | Controls final crystalline percentage, tensile strength, and flex life | Proportional damper and programmed cooling profile |
PROCESS CONTROL TIMELINE:
[Die Fill] --> [Rapid Ram Descent] --> [Controlled Compaction (300-500 kg/cm²)]
           --> [Pressure Dwell (15s-5m)] --> [Decompression (Step-Ramp)]
           --> [Hydraulic Soft Ejection] --> [Free Sintering at 370°C]
Advanced Troubleshooting & Defect Prevention
- Micro-Lamination & Delamination Cracks: Often caused by rapid decompression of trapped air or excessive preform compaction speed. Solution: Lower ram approach velocity to under 15 mm/s, implement stepped hydraulic decompression over 3–5 seconds, and check die vent clearance.
- Radial Out-of-Roundness & Warpage: Occurs when cooling rates through the 327°C to 300°C transition zone are non-uniform across the oven chamber. Solution: Ensure forced-air circulation velocity exceeds 2.5 m/s across all loading trays.
- Tensile Elongation Drop in Filled PTFE: Over-compaction of glass-filled or carbon-filled resins can fracture delicate reinforcing fibers. Solution: Calibrate specific compaction pressure to 380–420 kg/cm² and optimize punch landing clearances.
Machine Sizing & Tooling Integration
When engineering equipment for ptfe ball manufacturing process explained, calculate total press tonnage as:
Required Force (Ton) = (Projected Tool Area (cm²) × Compaction Pressure (kg/cm²)) / (1000) × 1.20 Safety MarginHEMSUN manufactures complete production lines—from 10 Ton compact gasket presses to 600 Ton multi-pillar automated compaction cells—equipped with Siemens/Schneider PLC touch screen interfaces, proportional hydraulic valving, and vacuum-hardened AISI D2 tooling.